


Stationery Rework vs Replacement: B2B Quality Control Decision Matrix

The decision between stationery rework and full batch replacement depends on defect severity, structural reversibility, and total landed cost. Modular issues like packaging relabeling, belly-band replacement, or external accessory insertion justify rework. In contrast, bound-core printing errors, spine adhesive failures, and raw material flaws demand full replacement to maintain structural integrity, protect brand equity, and eliminate downstream retail chargebacks.
What is the primary decision framework for stationery rework vs replacement?
When post-production quality control audits uncover non-conformities in paper goods, supply chain managers face a pivotal trade-off between corrective rework and full batch remanufacturing. The decision framework rests on four operational pillars: technical reversibility, unit economics, delivery timeline constraints, and channel compliance risk. Systematically assessing each pillar prevents costly trial-and-error repairs that damage delicate paper substrates or blow through critical distribution deadlines.
Technical reversibility assesses whether the non-conforming component can be physically altered or replaced without compromising the structural integrity or aesthetic standard of the finished stationery item. Paper is inherently hygroscopic, porous, and pressure-sensitive; disassembling a hardbound journal or Smyth-sewn book block often causes fiber tearing, spine warping, board delamination, or messy adhesive residue buildup. In such cases, attempting rework creates secondary flaws that degrade the finished product beyond commercial acceptance.
From an economic perspective, brands must balance the paper product quality inspection cost and manual rework labor against the scrap value and unit reproduction expenses. If manual sorting, bench repair, and repackaging exceed 30% to 35% of the initial unit manufacturing cost, or if labor-intensive handling introduces significant cosmetic fallout, full remanufacturing is usually the more cost-effective and predictable route.
Timeline constraints also heavily influence this operational choice. In seasonal retail programs—such as back-to-school campaigns, fourth-quarter holiday collections, or annual dated planner rollouts—a missed distribution center (DC) delivery window can trigger severe margin losses, late-delivery penalties, or immediate purchase order cancellations. Rework is only viable if localized sorting and correction can be completed well within the committed freight booking window.
Finally, channel risk dictates strict adherence to quality thresholds. Tier-one retail chains, national book retailers, and high-growth e-commerce platforms enforce zero-tolerance policies for defective merchandise. A notebook batch replacement decision is often the safest path to preserve vendor scorecards, maintain seller account ratings, and avoid catastrophic chargeback deductions when defect rates exceed Acceptable Quality Limit (AQL) tolerances.
Evaluation Metric | Rework Preferred | Replacement Required |
|---|---|---|
:--- | :--- | :--- |
Structural Impact | External or modular components (stickers, belly bands, polybags, shrink film) | Integral structural components (binding spine, sewn core, laminated cover board) |
Defect Dispersion | Isolated, lot-traceable, and below 3% occurrence rate | Systematic, raw-material related, or exceeding 10% occurrence rate |
Aesthetic Risk | Zero visible tool marks, fiber tearing, or adhesive residue | High probability of fiber tear, paper cockling, wrinkling, or scuffing |
Labor vs. Scrap Cost | Total rework cost remains below 30% of unit production cost | Total rework cost exceeds 40% of full batch reproduction cost |
Schedule Buffer | Correction fits comfortably within existing FOB or DDP transit buffers | Rework timeline delays vessel departure past the retail delivery cancellation date |
How do critical, major, and minor defects dictate stationery defect corrective action?
Formulating an effective stationery defect corrective action requires categorizing flaws according to standard AQL parameters (typically AQL 0 for Critical, AQL 1.5 or 2.5 for Major, and AQL 4.0 for Minor). Each tier directly informs whether rework or replacement is the compliant response, establishing clear boundaries for factory floor personnel and quality control teams.
Critical Defects (AQL 0.0): These non-conformities pose safety hazards, regulatory violations, or complete operational failure. Examples include sharp exposed wire ends on wire-o spirals, toxic ink formulations exceeding CPSIA lead or phthalate limits, broken needle fragments embedded in sewn journals, mold contamination in paper pulp, or missing mandatory country-of-origin labels. Critical non-conformities demand an immediate production halt. If the issue involves packaging or modular labeling, 100% sorting and rework may be permissible under tight supervision. If the hazard resides within the product substrate itself—such as contaminated raw paper pulp or non-compliant chemical coatings—the entire batch must be quarantined, destroyed, and remanufactured.
Major Defects (AQL 1.5 to 2.5): Flaws that impair structural durability, core usability, or primary commercial requirements. Examples include cracked spine hinges on hardcover notebooks, loose thread tension leading to signature separation, severe ink offset or text illegibility across printed planner spreads, missing dated folios, and expanding inner pockets that tear under light strain. For major structural defects, attempting manual repair almost always weakens the paper substrate. A notebook batch replacement decision is standard for major interior printing and binding failures, whereas outer slipcase or shrink-wrap misalignments can be reworked safely on secondary packaging lines.
Minor Defects (AQL 4.0): Cosmetic blemishes that do not affect the functional utility or structural longevity of the stationery item. Examples include superficial dust on shrink-wrapped gift boxes, slight die-cut corner burrs within 0.5 mm tolerances, minor hue variations across separate print runs, or lightly skewed barcode label placement on master packaging. Minor issues are typically addressed via localized rework: replacing outer polybags, wiping smooth plastic jackets, or re-applying external barcode stickers over defective prints.

Defect classification separates minor modular flaws suitable for rework from structural binding failures requiring batch replacement.
When is technical rework feasible for notebooks, planners, and retail paper packaging?
Technical feasibility depends on whether the defect is isolated within modular secondary packaging or embedded in the primary bound core. Understanding the engineering boundaries of paper, board, and adhesives helps quality assurance teams avoid counterproductive repairs that jeopardize retail acceptance.
Modular and Packaging Elements (High Feasibility for Rework)
Belly Bands and Sleeve Jackets: Defective artwork, misprinted barcodes, or damaged paper sleeves can be stripped and replaced without affecting the notebook. Clean removal and re-sleeving preserve the primary journal intact, making this one of the most cost-effective rework operations in paper converting.
Hangtags, Bookmarks, and Loose Accessories: Misplaced ribbon markers, detached elastic bands anchored via external eyelets, or missing foil stickers inside inner back pockets can be hand-assembled or repacked on a dedicated offline secondary assembly line without risking structural damage.
Outer Shrink-Wrapping and Corrugated Cartons: Scuffed shrink-wrap, damaged master shipper cartons, or incorrect pallet barcode labels are easily resolved through automated repackaging and relabeling protocols, ensuring compliance with distribution center intake requirements.
Interior Book Blocks and Binding Structures (Low Feasibility for Rework)
Casebound Hardcover Spine Delamination: When polyurethane (PUR) or EVA hot-melt adhesive fails to bond the folded signatures to the crash cloth or board spine, heating and reapplying glue creates thermal warping, paper cockling, and uneven endpaper wrinkling. Full replacement is necessary to guarantee durability.
Smyth-Sewn Core Assembly: Mis-collated calendar spreads or skipped folios in a Smyth-sewn planner cannot be repaired by slicing out individual leaves. Removing a single leaf compromises the thread tension of the entire paired signature, causing subsequent pages to loosen and detach during everyday use. The complete book block must be reprinted and rebound.
Spiral and Wire-O Perforations: Mis-punched pitch holes or torn edge margins cannot be patched or re-aligned. Attempting to re-punch wire-bound sheets leaves unsightly double-punched holes that compromise sheet retention and visual appeal.
Foil Stamping and Spot UV Registration Flaws: Misaligned foil stamping or bubbling spot UV varnish on laminated art paper covers cannot be stripped cleanly. Chemical solvents mar the matte or gloss lamination film, necessitating a complete cover reprint.
How does paper product quality inspection cost compare against rework labor and scrap value?
Every quality intervention involves direct and indirect expenditures. Balancing the paper product quality inspection cost, localized triage labor, raw material recovery, and freight implications yields an objective cost comparison model that guides financial and operational decision-making.
Calculating Inspection and Sorting Expenses
When a batch fails standard AQL sampling at factory exit or destination port entry, the immediate operational requirement is 100% piece-by-piece sorting. The total sorting inspection cost ($C_{sort}$) is calculated as:
$$C_{sort} = (N imes T_{unit} imes R_{labor}) + F_{handling}$$
Where $N$ represents the total lot size, $T_{unit}$ is the time required to inspect and grade each individual unit, $R_{labor}$ is the fully loaded hourly rate of the inspection staff, and $F_{handling}$ represents warehouse staging, destuffing, and pallet restacking fees. In North American or European distribution centers, third-party sorting rates often run between $35 and $65 per person-hour, quickly outstripping the original manufacturing labor cost incurred in overseas production facilities.
The Rework Financial Equation
Beyond initial sorting, the total cost of rework ($C_{rework}$) includes specialized offline labor, replacement packaging materials, machine re-setup, and potential scrap fallout generated during manual disassembly:
$$C_{rework} = C_{sort} + (N_{def} imes C_{mat}) + (N_{def} imes T_{fix} imes R_{labor}) + (N_{fallout} imes C_{unit})$$
Where $N_{def}$ is the number of defective units, $C_{mat}$ is the cost of auxiliary components (such as replacement belly bands, foil-stamped labels, or master cartons), $T_{fix}$ is the repair duration per unit, and $N_{fallout}$ accounts for units permanently damaged or soiled during manual handling.
The Replacement and Scrap Value Dynamic
Full batch remanufacturing ($C_{replace}$) involves raw material replenishment, high-speed automated printing and binding, and ocean or expedited air freight:
$$C_{replace} = (N imes C_{unit}) + Freight_{expedited} - Scrap_{recovered}$$
Paper scrap holds modest circular economy value; unprinted kraft and clean white offcuts can be baled and sold to local pulp mills. However, mixed-material scrap (such as foil-stamped board bonded with polyurethane covers or metal wire spirals) has negligible recovery value due to high segregation costs. When expedited air freight is required to meet tight retail launch windows, $C_{replace}$ increases significantly, making localized repackaging and modular rework the favored option whenever technically viable.

Modular packaging and labeling defects can be safely reworked without damaging the underlying notebook structure.
When is a full notebook batch replacement decision necessary to prevent retail chargebacks?
Mainstream retail chains, department stores, and global e-commerce platforms enforce strict vendor compliance guidelines. Violations trigger direct debit deductions, inventory disposal fees, and damaged vendor scorecards that threaten future shelf space allocations.
Channel-Specific Risks and Retail Chargeback Defect Control
Vendor Chargeback Vulnerability: Big-box retailers enforce automated chargeback schedules for barcode readability failures, master packaging dimension variances, incorrect carton labeling, and non-compliant pallet configurations. A single scuffed GS1-128 shipping container code or unreadable UPC on a notebook sleeve can trigger deductions from $5 to $25 per carton, plus administrative handling fees that rapidly erode gross margins.
Structural Failures on Retail Shelves: Notebooks that exhibit warped hardcovers, bowing covers caused by improper paper moisture balancing, or cracked spines under customer handling lead to elevated in-store return rates. Retailers regularly debit suppliers for the full retail value of returned goods, accompanied by return logistics surcharges.
E-Commerce Account Suspensions: On Amazon and other DTC marketplaces, customer reviews citing missing planner dates, bleeding fountain-pen ink, or split journal spines can trigger the suspension of a high-ranking ASIN. Once an e-commerce listing is locked for high return rates, the lost sales rank and advertising equity often cost far more than remanufacturing the defective inventory.
Implementing strict retail chargeback defect control requires knowing when to halt a compromised shipment at the factory gate. If a defect involves internal page collations, missing FSC certification chain-of-custody tracking numbers, or incorrect barcode printing, executing a notebook batch replacement decision before the goods depart the factory is far less costly than managing reverse logistics, warehouse sorting fees, and chargeback claims at a destination distribution hub.
How can dual-site process controls and root-cause CAPA prevent recurring batch defects?
Corrective and Preventive Action (CAPA) systems resolve the root causes of production non-conformities rather than merely treating visible symptoms. Using an integrated dual-site manufacturing network allows paper goods brands to combine agile engineering with reliable volume production.
Dual-Site Synergy for Quality Assurance
Lion Paper utilizes an integrated supply-chain model across two specialized facilities:
Jiaxing, China Facility (3,000 sqm): Operates as the central hub for product planning, structural engineering, rapid prototyping, and prepress proofing. High-precision prepress calibration, computerized color-matching profiles, and pilot sample testing take place here before mass production begins.
Cambodia Facility (10,000 sqm): Built for scalable mass production, automated line converting, and cost-effective bulk assembly. It delivers an annual output exceeding 5 million notebook units with standardized standard operating procedures (SOPs).
By qualifying technical dies, paper grammage tolerances, and adhesive selections in the Jiaxing prototyping center, mass manufacturing in Cambodia runs with established setup parameters, significantly lowering baseline defect risks across volume orders.
Four-Phase CAPA Execution Framework
To ensure systematic resolution of quality issues, a structured four-phase CAPA workflow is deployed across production sites:
Phase 1: Immediate Containment (0 to 24 Hours)
Quarantine affected production lots in the dual-site staging area.
Freeze related raw materials, including paper reels, adhesives, and cover boards.
Issue an immediate containment notice to all quality control shift supervisors.
Phase 2: Root-Cause Investigation (24 to 48 Hours)
Deploy Ishikawa (Fishbone) analysis across the 5Ms (Man, Machine, Material, Method, and Measurement).
Test fiber grain direction, paper moisture content (maintaining a target range of 5.5% to 6.5%), and adhesive viscosity.
Cross-reference production lot numbers with raw material supplier mill test certificates.
Phase 3: Corrective Action Implementation (Day 3 to Day 5)
Recalibrate automated line mechanical tolerances, blade sharpness, and spine heating temperature settings.
Update visual defect catalogs (Defect Atlas) at all in-line and end-of-line manual inspection stations.
Enforce mandatory signature pull-force tensile testing, requiring values greater than 4.5 N/cm.
Phase 4: Preventive Standardization and Verification (Day 6 to Day 30)
Audit standard operating procedure (SOP) compliance across prepress and mass assembly lines.
Perform follow-up AQL 1.0 tightened sampling on three consecutive production runs.
Log all CAPA outcomes and machine parameters in the vendor compliance archive for future replenishment runs.
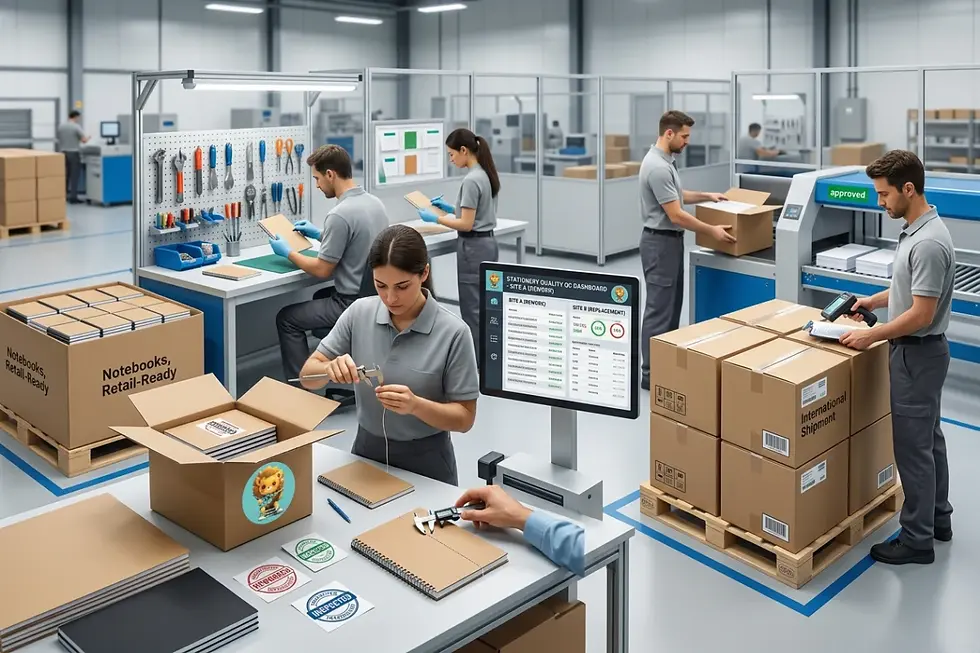
Standardized final carton inspections and barcode verification protect stationery brands from downstream retail chargebacks.
What actionable QC checklist ensures supplier alignment and retail chargeback defect control?
To ensure consistent quality across notebook lines, planners, and office paper stationery, procurement and QA managers should include a comprehensive quality agreement in their initial RFQ specifications.
Raw Material Specifications: Define baseline paper standards, including basis weight in grams per square meter (gsm), bulk caliper thickness, ISO brightness percentage, fiber grain direction parallel to the binding spine, and internal moisture content (5.5% to 6.5%). Explicitly require FSC-certified chain-of-custody tracking where environmental sustainability claims are required.
Binding and Structural Integrity Metrics: Mandate minimum page-pull tensile strengths (greater than 4.0 N/cm for perfect-bound journals; greater than 5.5 N/cm for Smyth-sewn book blocks). Define flex-durability limits for cover spine hinges to prevent creasing after repeated 180-degree lay-flat openings.
Color Fastness and Print Registration: Set maximum allowable Delta-E color variance thresholds (typically Delta-E less than 2.0) against approved digital press proofs. Require spot UV and foil stamping registration to stay within plus or minus 0.3 mm of printed background elements.
Defect Classification Catalog (Defect Atlas): Provide visual boundary boards highlighting acceptable versus non-acceptable limits for glue squeeze-out, thread tail length (maximum 2.0 mm), corner wrap rounding, and ribbon marker heat-sealed edge fraying.
Retained Golden Sample Protocol: Require three sets of signed, identical pre-production golden samples: one retained at the brand office, one at the Jiaxing engineering hub, and one at the Cambodia production facility. All final AQL inspections must match these samples.
Packaging and Barcode Verification: Verify 100% of retail master carton shipping marks and item UPC barcodes using an ISO/IEC 15416-compliant barcode verifier with a minimum Grade B verification score.
Balancing rework feasibility against batch replacement protects your supply chain from cost overruns, delivery delays, and customer dissatisfaction. Aligning structural engineering, clear AQL defect limits, and cross-border manufacturing controls helps consumer brands maintain consistent quality across all retail channels. Share defect photos/data, return reasons, chargeback criteria, inspection rules and volumes with Lion Paper for a corrective-action and QC review.
FAQ
What is the typical AQL standard used for notebook and stationery manufacturing?
Most international stationery brands and retail buyers follow ANSI/ASQ Z1.4 (ISO 2859-1) Level II Normal Sampling, applying AQL 0 for Critical defects (safety and regulatory compliance), AQL 1.5 or 2.5 for Major defects (structural and functional integrity), and AQL 4.0 for Minor defects (minor cosmetic imperfections).
Can delaminated hardcover notebook spines be repaired using heat reactivation?
Heat reactivation is generally not recommended for hardcover books. Reheating polyurethane (PUR) or EVA hot-melt adhesives often causes thermal cockling of the paper, board warping, and uneven endpaper wrinkling, creating secondary cosmetic flaws that compromise retail quality.
How does Lion Paper handle defect prevention across its China and Cambodia facilities?
Lion Paper uses its 3,000 sqm Jiaxing hub for design, engineering, and prepress proofing to validate specifications, then transitions mass production to its 10,000 sqm Cambodia facility. Standardized SOPs, unified defect catalogs, and rigorous in-line inspections maintain consistent quality across both sites.
What is the fastest way to resolve an unexpected barcode scanning failure on delivered cartons?
If the underlying product is unaffected, the most practical approach is localized relabeling. High-opacity thermal transfer barcode labels that meet ISO/IEC Grade A or B standards can be applied directly over defective barcodes at the destination warehouse, avoiding the high cost of a full product reprint.


Comments